Bar to Annealed tube
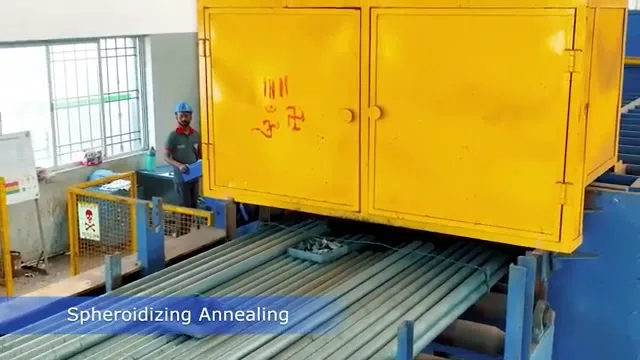
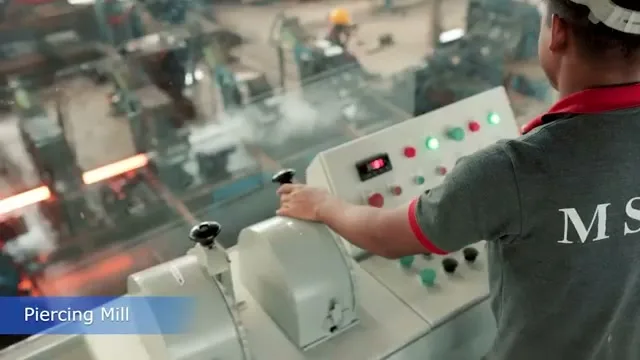
Two induction heaters feed the piercing mills which turns billets to first hollow tube, followed by over 100 meter continuous furnace with N₂ atmosphere for spheroidizing annealing.
Full process from Raw Material Inspection to Finish Tube dispatch all in-house.
The plant processes mother tubes and final tubes in-house, with mother tubes made from bars. All-electric induction heating, controlled N₂ annealing and in-line NDT keep the route under one roof.
 Piercing mill
Each stage is listed with a concise explanation.
A five-head cutting system prepares round bar to the required starting length.
Two induction heaters bring the bar to forming temperature before piercing.
A over 100 meter long continuous furnace with N₂ atmosphere, conditions the bearing steel to be in a soft-annealed condition.
Prepare the tube surface for stable downstream processing and finished quality.
Pilger mills and Draw benches reduce and control the tube geometry to size.
Stress-relieve, straighten, end-cut and part the tube for handling and application.
Rotary ultrasonic testing and automatic Eddy Current Testing inspect every tube, with heat-number traceability.
Complete the visible finishing route, identify finished lots and prepare them for dispatch.
Purpose-built equipment keeps heating, forming, cold work and inspection connected.
Two induction heaters feed the piercing mills which turns billets to first hollow tube, followed by over 100 meter continuous furnace with N₂ atmosphere for spheroidizing annealing.
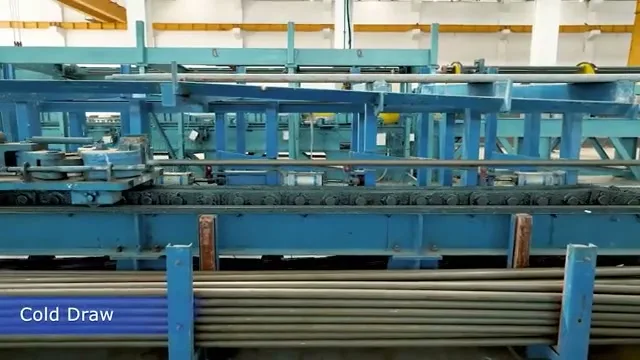
Twenty-two cold-roll pilger machines, and three draw benches, support controlled final tube geometry.
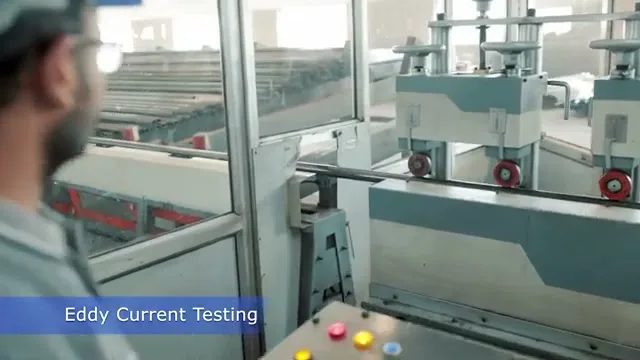
Two ultrasonic machines use 16-probe rotary UT alongside automatic Eddy Current Testing for 100% NDT.
Send the tube OD, material, length, annual volume and end-use. The enquiry form is designed around the information engineering teams actually need.